MEP Coordination in Precast Concrete Structures: Openings, Sleeves & Embedded Services
Precast concrete construction offers speed, precision, and quality control — but it demands one thing above all else: early, thorough MEP coordination. Unlike cast-in-place construction, precast elements are manufactured off-site in a controlled factory environment. Once a panel or beam leaves the plant, its geometry is locked. Any electrical conduit, plumbing sleeve, HVAC penetration, or structural blockout that was missed during the design and shop drawing phase must be added through costly field drilling, coring, or cutting — all of which compromise structural integrity, delay the schedule, and inflate project budgets.
Why MEP Coordination Is Essential in Precast Construction
The Precast Constraint
Precast elements — wall panels, double tees, hollowcore slabs, columns, and beams — are precision-engineered products. Their reinforcement layouts, lifting insert locations, camber calculations, and connection details are all finalized during the shop drawing phase.
Introducing a 6-inch sleeve or a 12-inch blockout after fabrication is not simply inconvenient — it may require re-engineering the element, adding supplemental reinforcement, or in worst cases, scrapping and remanufacturing the piece entirely.
Early MEP coordination eliminates these risks by embedding service penetrations directly into the precast production process, treating them as first-class structural features rather than afterthoughts.
The Cost of Getting It Wrong
According to industry benchmarks, MEP-related rework in precast projects accounts for 3–7% of total project cost when coordination is deferred to the construction phase. Proactive coordination consistently reduces this to under 1%.
Cost Multiplier
Field drilling vs. cast-in sleeve cost ratio
Rework Cost
Of total project cost lost to poor MEP coordination
Issues Preventable
Of field conflicts resolved by early BIM coordination
Faster RFI Resolution
When clash detection is performed in design phase
Successful precast projects treat MEP penetrations, sleeves, blockouts, embeds, and service routes as design inputs rather than field changes. Every coordinated opening captured during detailing reduces risk, preserves structural integrity, and protects both schedule and budget.
MEP coordination is not a downstream construction activity. In precast construction, it is a core detailing responsibility that determines manufacturability, structural performance, schedule reliability, and project profitability.
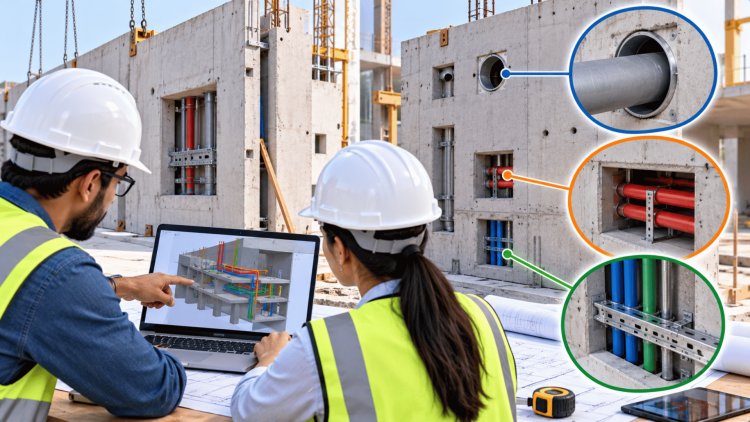
The first step in any precast MEP coordination workflow is a disciplined, discipline-by-discipline audit of every service that must pass through or be embedded within a precast element. This audit should occur before shop drawings are released for approval and must involve the structural engineer of record, the precast fabricator's detailer, and all MEP subcontractors working from coordinated BIM models.
Electrical conduits, cable trays, pull boxes, and junction boxes must be mapped against every precast panel and slab. EMT and rigid conduit sleeves are cast directly into panels during fabrication. Locations must respect minimum edge distances (typically 6–8 inches from panel edges) and must not conflict with lifting anchors or connection hardware. Electrical engineers should provide conduit routing plans in 3D BIM format no later than 60% design development.
Domestic water, sanitary, storm, and specialty piping systems frequently require largediameter penetrations through load-bearing precast elements. Drain lines in particular often cross hollowcore planks at angles, requiring non-rectangular blockouts that must be carefully sized and reinforced with trimmer bars. All plumbing penetrations should be coordinated with the structural engineer to verify that web-cutting limits for hollowcore are not exceeded.
Large ductwork penetrations represent the highest-risk MEP conflicts in precast coordination. Rectangular blockouts for duct penetrations in shear walls or spandrel panels must be evaluated for their effect on lateral load paths. HVAC engineers must finalize duct routing and size selections — including insulation and liner dimensions — before coordination drawings are issued, since undersized blockouts are extremely costly to remedy post-fabrication.
Round sleeves: Use schedule 40 PVC or galvanized steel pipe forms; specify inside diameter 1–2 inches larger than the service to allow for insulation and installation tolerance
Rectangular blockouts: Use plywood or foam block forms secured to the form bed; add supplemental trimmer reinforcement around all four sides per structural engineer's detail
Fire-rated assemblies: All through-penetrations must include ULlisted firestop sleeve details coordinated with the fire protection engineer
Tolerances: PCI MNL-135 recommends ±½ inch location tolerance for sleeves in precast panels; MEP subcontractors must design connections to accommodate this
Hanger inserts: Beam clamps and cast-in coil inserts for MEP hangers must be located in the precast shop drawings and confirmed against pipe/duct routing in BIM
Embedded conduit: Conduit cast into precast elements must not reduce the structural cross-section by more than 1/3 of the slab thickness and must maintain minimum 1.5-inch concrete cover
Waterstop and sealants: Wet-area penetrations require waterstop integration at the sleeve/concrete interface, specified by the waterproofing consultant
Documentation: Every sleeve, blockout, and insert must appear on a dedicated MEP/Precast Coordination Drawing, referenced on both the structural and MEP permit drawings
Identifying Penetrations & Detailing Sleeves, Blockouts, and Cast-In Inserts
Electrical Penetrations
Plumbing & Drainage
HVAC & Mechanical
Sleeve, Blockout & Insert Detailing Standards
Sleeves & Blockouts
Cast-In Inserts & Embedded Plates
One of the most technically demanding aspects of precast MEP coordination is ensuring that service openings do not compromise the structural performance of the precast element. Every opening—no matter how small—interrupts the flow of forces through the concrete cross-section and must be evaluated by the structural engineer of record. The coordination team must understand the structural implications before finalizing any opening location.
Federated models, structured clash detection, EOR approval, and IFC shop drawing integration protect structural performance while enabling coordinated MEP routing.
Coordinating Reinforcement
with Service OpeningsZero unresolved clashes before any element enters the production queue.
The ultimate measure of successful MEP coordination in precast construction is a field installation that proceeds exactly as planned — no unscheduled coring, no emergency RFIs, no structural patches, and no schedule delays caused by missing or mislocated openings. Achieving this standard requires discipline, early engagement, and a culture of coordination that spans the entire project team.
The earlier MEP routing decisions are locked, the more cost-effectively they can be incorporated into precast production. Even conceptual duct and pipe routing in SD phase allows the structural engineer to begin evaluating opening impacts before the reinforcement design is finalized. Projects that begin precast/MEP coordination after design development are already behind.
Engage the precast fabricator as early as possible — their detailers understand panel production constraints that are invisible in the design model.
Clash detection is only as reliable as the models being tested. Require all MEP subcontractors to model systems at LOD 400 — including insulation, hangers, fittings, and access clearances — before coordination meetings.
A duct modeled without insulation will pass a clash test but fail in the field. Establish model quality checkpoints in the BIM Execution Plan and enforce submission deadlines contractually.
Establish a formal MEP Routing Freeze milestone as a contractual prerequisite to the precast shop drawing approval process. Changes to pipe sizes, duct routing, or equipment locations after this freeze must go through a formal change management process with cost and schedule impact analysis.
This single contractual mechanism prevents the majority of late-coordination conflicts that plague precast projects.
Coordination does not end when shop drawings are approved. Weekly MEP/precast coordination meetings should continue through the fabrication phase to manage any design changes, substitution requests, or field condition discoveries that may affect embedded elements.
The fabricator's project manager should be a standing attendee with authority to flag production conflicts in real time.
Upon erection of each precast element, the MEP coordination team should perform a physical verification check against the coordinated BIM model using a tablet-based field app (e.g., Autodesk BIM 360 Field, PlanGrid, or Procore).
Verify sleeve locations, check that cast-in inserts are accessible and undamaged, and confirm that no field modifications are being made without engineering approval. Any discrepancy between the as-built and the coordinated model should be logged as a field coordination issue and resolved before MEP rough-in begins in that zone.
Maintain a complete MEP/Precast Coordination Log throughout the project — a living document that tracks every opening, insert, and embed from initial request through shop drawing approval, fabrication confirmation, and field verification.
At project closeout, this log forms the basis of the as-built documentation package, which is critical for future renovations, tenant fit-outs, or structural modifications. Projects with strong coordination documentation routinely command higher asset values and experience fewer issues during building life-cycle management.
For teams looking to implement these workflows on their next project, explore practical guidance on precast BIM coordination services and MEP clash detection workflows available through Digiverse Studio's project delivery resources.
Successful MEP coordination in precast structures is not a phase — it is a continuous, team-wide discipline that begins at concept design and ends only when every sleeve, blockout, and embedded insert is verified in the field. Zero field modifications is not an aspirational goal; it is the achievable standard when coordination is treated as a first-priority deliverable.
Avoiding Costly Field Modifications: Best Practices & Key Takeaways
Start Coordination at Schematic Design
Mandate LOD 400 BIM Models from All Trades
Freeze MEP Routing Before Shop Drawing Release
Conduct Weekly Coordination Meetings Through Fabrication
Field Verification Protocol
Documentation & Closeout
Zero field modifications are achieved long before erection begins. They are the result of disciplined BIM coordination, early routing decisions, controlled change management, rigorous verification, and complete documentation throughout the entire precast project lifecycle.
What's Your Reaction?